Manufacturing Water Leak Detection: Prevent Production Downtime in 2026
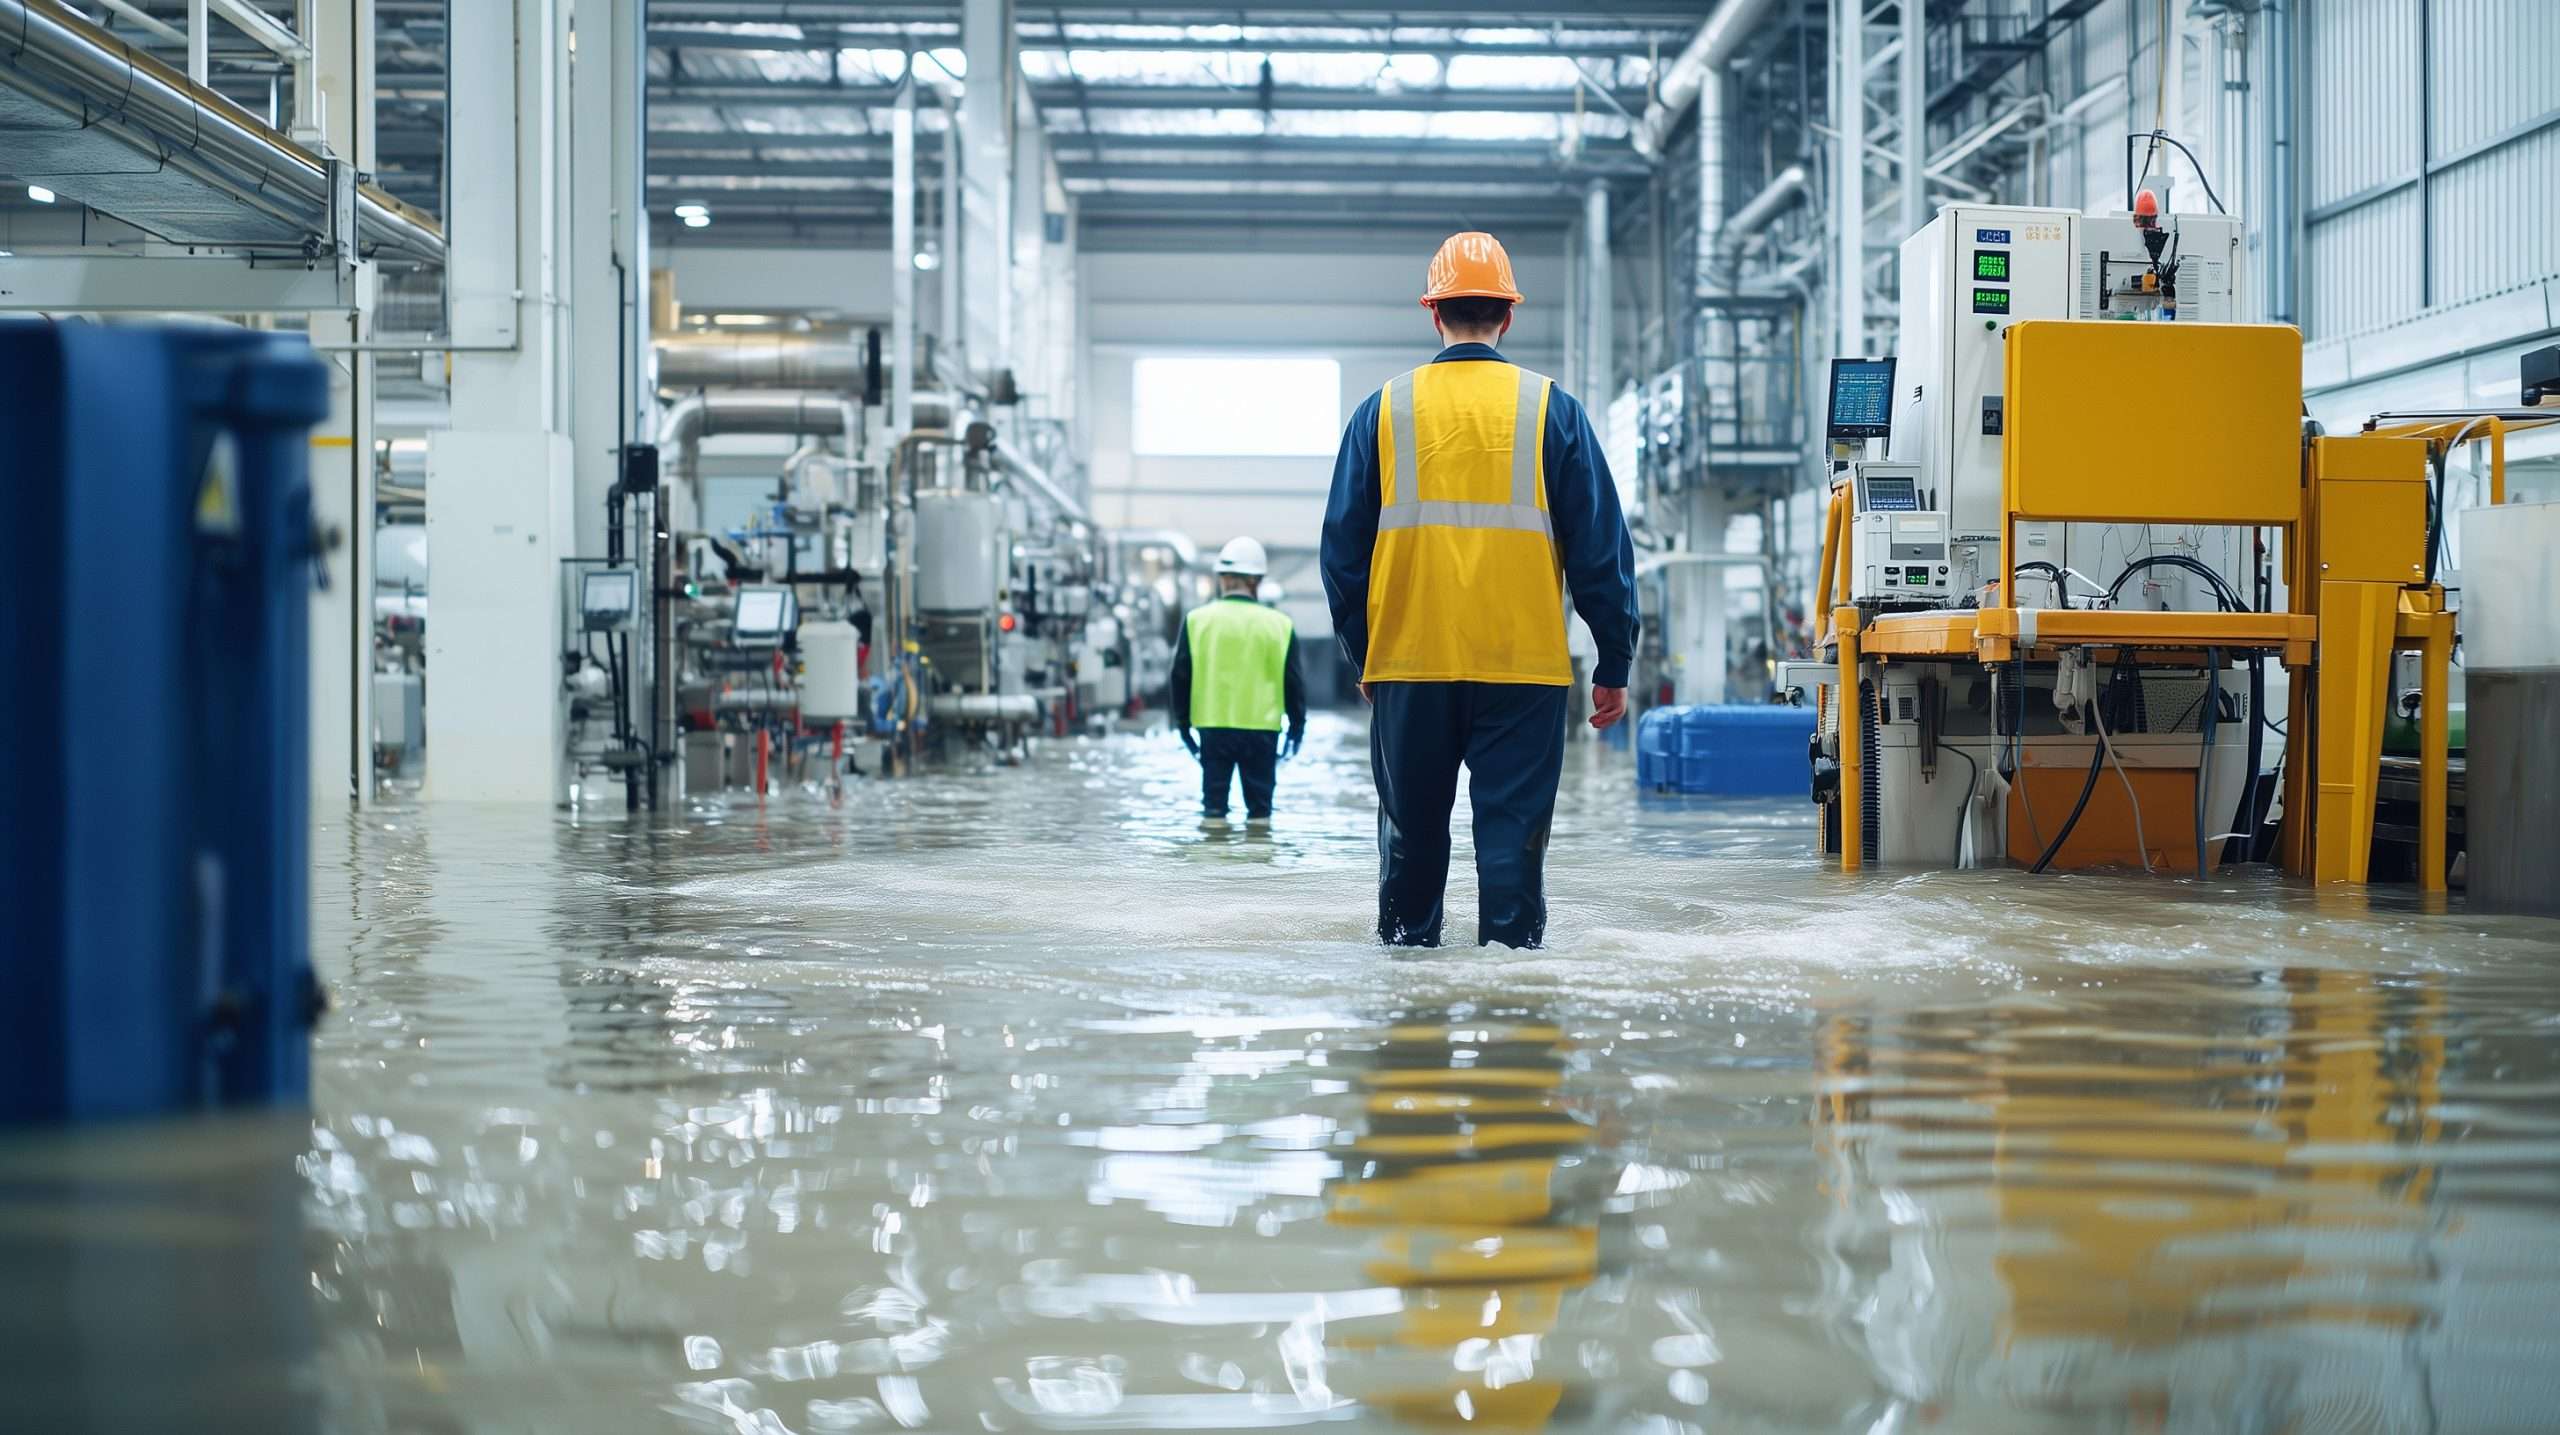
Water damage represents one of the most significant and underestimated threats to manufacturing operations. When water infiltrates production areas, the consequences extend far beyond immediate cleanup costs to include equipment damage, production downtime, inventory losses, and potential mold remediation that can close facilities for weeks. Manufacturing facilities face unique vulnerabilities due to the concentration of high-value equipment, the presence of multiple water sources from process systems to fire suppression, and the catastrophic cost of production interruptions. Manufacturing water leak detection systems provide the early warning capability that transforms potential disasters into manageable maintenance events, protecting both physical assets and operational continuity.
Manufacturing facilities face extraordinary financial exposure from water damage events. With average downtime costs reaching $260,000 per hour across the manufacturing sector, even brief production interruptions translate into substantial losses. Water and oil leaks rank among the leading causes of unplanned machine downtime, contributing to the $50 billion industrial manufacturers spend annually addressing unexpected equipment failures. The automotive industry experiences the most severe impacts, with downtime costs reaching $2.3 million per hour at major assembly plants. Beyond immediate production losses, water damage creates cascading effects including supply chain disruptions, quality control failures, and potential contract penalties that amplify initial damage costs by factors of three to five. Manufacturing water leak detection systems provide the early warning capability that transforms potential catastrophes into manageable maintenance events.
Manufacturing water leak detection delivers immediate protection against costly production downtime and equipment damage.
Average Manufacturing Downtime Cost
Mold Growth Begins After Water Exposure (EPA)
Average Implementation Timeline
This comprehensive guide examines how manufacturing water leak detection technology protects manufacturing operations from costly water damage events. We explore the specific vulnerabilities manufacturing facilities face, the detection technologies available for industrial environments, implementation strategies that minimize production disruption, and the return on investment calculations that make leak detection a financial imperative for manufacturing operations. Whether operating a small machine shop or a multi-building industrial campus, understanding how early leak detection prevents production downtime enables informed decisions about protecting critical manufacturing assets.
Water Damage Risks in Manufacturing Facilities
Manufacturing environments contain numerous water sources that create leak risks throughout the facility. Process water systems, cooling loops, hydraulic equipment, fire suppression systems, HVAC condensate, and domestic plumbing all represent potential failure points. Unlike office buildings where water damage primarily affects finishes and furnishings, manufacturing water damage directly threatens production equipment worth millions of dollars, raw materials and work-in-progress inventory, and the facility’s ability to fulfill customer orders. Understanding these risks provides the foundation for effective manufacturing water leak detection system design.
Process water systems present particularly significant risks in manufacturing environments. Many manufacturing processes require water for cooling, cleaning, chemical dilution, or direct incorporation into products. These systems operate under pressure and often run continuously, meaning failures can release substantial water volumes before anyone notices the problem. A single industrial cooling system might circulate thousands of gallons per hour, and pipe failures or fitting leaks can flood production areas within minutes. Manufacturing water leak detection sensors positioned at key points throughout process water systems provide immediate notification when leaks occur, enabling rapid response before water spreads to sensitive equipment.
Hydraulic systems represent another major water damage risk category, though the damage involves oil rather than water. Manufacturing facilities relying on hydraulic presses, injection molding machines, or hydraulic material handling equipment face similar leak detection requirements. Hydraulic fluid releases create slip hazards, environmental contamination, and equipment damage comparable to water leaks. Many facilities implement combined water and oil leak detection systems that protect against both hazard types using similar sensor technologies.
Fire suppression systems create paradoxical risks in manufacturing facilities. While essential for fire safety, sprinkler systems and fire suppression equipment can cause substantial water damage when they malfunction or activate accidentally. Frozen sprinkler pipes during winter months represent a common failure mode, particularly in facilities with inconsistent heating in warehouse areas, loading docks, or unoccupied sections. A single sprinkler head failure can release 20-50 gallons per minute, flooding production areas rapidly. Manufacturing water leak detection systems that monitor sprinkler risers and fire suppression equipment provide early warning of freezing conditions or system failures before catastrophic water release occurs.

Undetected water leaks in manufacturing facilities can cause millions in equipment damage, production losses, and mold remediation costs.
Manufacturing Water Leak Detection Technologies
Modern manufacturing water leak detection systems offer multiple sensor technologies suited to different manufacturing applications. Point sensors detect water presence at specific locations, making them ideal for placement beneath equipment, at drain locations, or in areas where leaks would first appear. Rope sensors can monitor extended linear distances such as pipe runs, cooling system perimeters, or equipment galleries where leak locations cannot be predicted precisely. Flow monitoring systems detect abnormal water consumption patterns that indicate leaks anywhere in the distribution system. Understanding these technologies enables manufacturing facilities to design comprehensive manufacturing water leak detection coverage tailored to their specific risks.
Point sensors represent the most common manufacturing water leak detection technology deployed in manufacturing facilities. These compact devices detect water contact and immediately transmit alerts through wired or wireless connections to central monitoring systems. Modern point sensors operate on battery power with multi-year battery life, eliminating the need for electrical connections at each sensor location. Wireless communication protocols enable rapid deployment without disrupting production activities. Manufacturing facilities typically deploy point sensors beneath CNC machines, near hydraulic power units, under HVAC equipment, at water heater locations, and anywhere water damage would create significant consequences.
Rope sensors provide continuous leak detection along extended paths, making them valuable for manufacturing applications where leak locations cannot be predicted. A single rope sensor can monitor 50-200 feet of linear distance, detecting water contact anywhere along its length while identifying the approximate leak location. Manufacturing facilities deploy rope sensors around process water equipment perimeters, along pipe runs in utility corridors, beneath raised flooring in control rooms, and around the bases of tanks or vessels. Rope sensors prove particularly effective in manufacturing environments because they adapt to irregular equipment layouts and can be routed around obstacles that would prevent point sensor placement.
Flow monitoring systems provide complementary leak detection capability by identifying abnormal water consumption patterns. These systems attach to water meters or install inline to measure water flow continuously. When consumption exceeds normal patterns indicating a leak somewhere in the distribution system, the monitoring system generates alerts. Flow monitoring proves particularly valuable for detecting leaks in concealed piping that point sensors cannot monitor directly. Manufacturing facilities with extensive underground or in-wall piping benefit from flow monitoring as a detection layer that supplements point and rope sensors at visible locations. Combining flow monitoring with energy monitoring systems provides comprehensive utility oversight.
Manufacturing-Specific Water Leak Detection Challenges
Manufacturing environments present unique challenges for manufacturing water leak detection that require careful consideration during system design. Industrial noise, electromagnetic interference, temperature extremes, and chemical exposure can affect sensor performance if equipment selection does not account for these conditions. Production schedules and continuous operations limit opportunities for installation and maintenance activities. Multi-shift operations require alert notification systems that reach responsible personnel regardless of time or day. Successfully deploying manufacturing water leak detection requires addressing each of these challenges during the planning phase.
Environmental conditions in manufacturing facilities often exceed parameters typical for commercial buildings. Temperature extremes near furnaces, ovens, or refrigerated storage areas affect sensor battery life and electronic performance. Humidity levels in facilities with process water systems or wash-down operations may challenge sensor durability. Chemical exposure in plating shops, paint facilities, or chemical processing areas can damage sensors not designed for industrial environments. Selecting industrial-grade manufacturing water leak detection equipment rated for the specific environmental conditions present in each facility area ensures reliable long-term performance.
Electromagnetic interference from motors, drives, welding equipment, and industrial controls can disrupt wireless sensor communications in manufacturing facilities. Facilities with extensive metal structures, equipment housings, and racking may experience wireless signal attenuation that affects communication reliability. Manufacturing water leak detection systems designed for industrial applications address these challenges through robust wireless protocols, mesh networking that routes around obstacles, or wired communication options for challenging locations. Site surveys during the design phase identify areas requiring special attention and inform equipment selection decisions.
Modern leak detection systems integrate with building automation systems, manufacturing execution systems, and enterprise monitoring platforms. Integration enables automated responses when leaks occur, such as shutting off water supply valves, stopping nearby equipment to prevent damage, or activating sump pumps. Alert notifications can route through existing manufacturing communication systems to reach operators, maintenance personnel, and management through appropriate channels. Integration with temperature monitoring systems provides comprehensive environmental protection.
Protect Your Manufacturing Investment
Learn how manufacturing water leak detection can prevent costly production downtime at your facility.
Implementing Manufacturing Water Leak Detection
Successful manufacturing water leak detection implementation begins with comprehensive risk assessment. This assessment identifies water sources throughout the facility, evaluates potential damage consequences at each location, prioritizes protection for high-value equipment and critical production areas, and documents existing conditions for insurance purposes. Risk assessment typically involves facility walkdowns with maintenance, operations, and engineering personnel who understand where water problems have occurred historically and where unprotected vulnerabilities exist. The assessment output guides sensor placement decisions and system design specifications.
Phased implementation approaches enable manufacturing facilities to deploy leak monitoring without disrupting production. Initial phases typically focus on highest-risk areas including electrical rooms, server rooms, control system enclosures, and areas containing irreplaceable equipment. Subsequent phases extend coverage to production equipment, process water systems, and support areas. Phased approaches also allow staff to develop familiarity with system operation and response procedures before expanding coverage. Many facilities begin with pilot installations in selected areas to validate equipment performance and refine installation techniques before broader deployment.
Installation timing in manufacturing facilities often aligns with production schedules, planned shutdowns, or maintenance windows. Wireless sensor installation proceeds rapidly since no wiring is required, enabling deployment during shift changes, lunch breaks, or brief production pauses. Wired installations for sensors in areas with communication challenges may require longer windows coordinated with maintenance schedules. Gateway and communication equipment installation typically occurs in non-production spaces without affecting operations. Professional installation services familiar with manufacturing environments complete deployments efficiently while maintaining required safety protocols.
Manufacturing Water Leak Detection ROI
Manufacturing water leak detection systems deliver compelling return on investment for manufacturing facilities through multiple value streams. Direct damage prevention represents the most significant benefit, with detected leaks typically causing under $50,000 in damage compared to $500,000 or more for undetected leaks that spread over hours or days. Insurance premium reductions of 5-15% reward facilities that demonstrate proactive risk management through manufacturing water leak detection deployment. Avoided production downtime prevents revenue losses that dwarf equipment repair costs. These combined benefits typically generate positive ROI within 12-24 months of system installation.
Calculating avoided damage costs requires considering the full scope of potential losses. Equipment repair or replacement costs represent only the beginning. Production downtime during repairs often exceeds equipment costs, particularly in high-value manufacturing operations. Expedited shipping for replacement parts and overtime labor for accelerated repairs add substantial costs. Customer penalties for late deliveries, lost future orders from damaged relationships, and market share losses to competitors who fulfill demand during outages multiply direct losses. Many manufacturing facilities that experience significant water damage never fully recover their competitive position.
Insurance benefits from manufacturing water leak detection extend beyond premium reductions. Documentation provided by monitoring systems supports insurance claims with precise information about when damage began, how it progressed, and what response actions occurred. This documentation typically accelerates claim processing and reduces disputes about damage extent or cause. Some insurers now require manufacturing water leak detection as a condition of coverage for high-value manufacturing facilities, recognizing that monitoring dramatically reduces claim frequency and severity.
Comprehensive monitoring approaches that combine manufacturing water leak detection with temperature monitoring and other environmental sensors provide enhanced ROI through shared infrastructure and consolidated monitoring. Temperature monitoring protects against frozen pipe risks, refrigeration failures, and process temperature excursions. Combined platforms reduce per-sensor costs through volume deployment, simplify system management through unified interfaces, and provide comprehensive protection. The Monitoring as a Service approach enables manufacturing facilities to deploy comprehensive protection with predictable monthly costs rather than large capital expenditures.

Envigilance water leak detection dashboard provides real-time monitoring and instant alerts for manufacturing facilities.
Response Protocols When Water Leak Detection Sensors Trigger
Effective leak detection requires defined response protocols that ensure rapid action when sensors detect water. Response protocols should specify who receives alerts, through what communication channels, and what actions each person should take. First responders need clear guidance on locating the affected area, assessing the situation, and taking immediate protective actions. Escalation procedures should define when to involve maintenance supervision, facility management, or emergency services. Documentation requirements ensure that response actions are recorded for insurance purposes and post-incident analysis.
Immediate response actions when water leak detection systems alert typically include locating and stopping the water source, protecting nearby equipment and materials, and notifying appropriate personnel. Shutting off water supply valves prevents additional water release once a leak is identified. Moving equipment, materials, or inventory away from spreading water limits damage extent. Deploying wet vacuums, pumps, or absorbent materials begins water removal. These immediate actions can occur within minutes of leak detection, dramatically reducing damage compared to situations where leaks continue for hours before discovery.
Secondary response activities address longer-term damage prevention and documentation needs. Dehumidification equipment deployment begins drying affected areas to prevent mold growth within the critical 24-48 hour window. Photography and video documentation of damage extent supports insurance claims and identifies repair requirements. Assessment of affected equipment determines whether items can be cleaned and returned to service or require replacement. Notification of insurance carriers begins the claims process. Investigation into leak causes identifies repairs needed to prevent recurrence.
Automated response capabilities enhance leak monitoring effectiveness in manufacturing facilities. Integration with building automation enables automatic water shutoff when sensors detect leaks, limiting water release even before personnel respond. Automated alerts through multiple channels including text messages, phone calls, emails, and facility alarm systems ensure responsible personnel receive notification promptly. Integration with security systems can trigger cameras to record affected areas. Automated logging of sensor status, alert times, and response actions creates documentation without requiring manual record-keeping during emergency response.
Case Study: Oklahoma Manufacturing Plant Flood (May 2019)
Incident: When torrential rains caused the Arkansas River to reach historic levels in May 2019, levees overtopped and flooded several areas of Oklahoma. Among those impacted was a 160-acre manufacturing facility that experienced approximately three feet of contaminated floodwater throughout the entire plant. The water affected control cabinets, electrical distribution systems, and CNC machines across the facility.
Challenges: The severity of flooding prevented facility access for approximately two weeks, during which submerged equipment suffered accelerated corrosion damage. Equipment affected included Okuma CNC lathes, Bronx Engineering control cabinets, OMAX waterjet cutters, and electrical switchgear. Most equipment was custom-manufactured with replacement lead times of 9-12 months.
Outcome: Restoration specialists successfully restored 100 percent of eligible equipment in three weeks, preventing what would have been nearly a year of production shutdown waiting for replacement equipment. Submerged electronics and dry transformers required replacement, but the rapid response prevented total equipment loss.
Prevention Insight: While this case involved external flooding rather than internal leaks, it demonstrates the devastating impact of water on manufacturing equipment. Water leak detection systems with automatic shutoff capabilities can prevent internal water sources from causing similar damage, protecting CNC machines, control cabinets, and electrical systems from water exposure that leads to corrosion and equipment failure.
Source: AREPA Equipment Restoration Case Study, 2019 Arkansas River Floods
Manufacturing Water Leak Detection: Frequently Asked Questions
How quickly can water leak detection systems identify leaks in manufacturing facilities?
Modern water leak detection systems identify leaks within seconds of water contacting sensors. Alert transmission occurs immediately, with notifications reaching designated personnel within 1-2 minutes of detection.
This rapid detection enables response times of 8-12 minutes compared to 2-4 hours or longer when leaks are discovered through routine observation. In manufacturing facilities where downtime costs reach $260,000 per hour, the difference between minute-scale and hour-scale detection translates directly into hundreds of thousands of dollars in avoided losses.
What types of water leaks can detection systems identify in manufacturing environments?
Water leak detection systems in manufacturing environments identify leaks from multiple sources including process water systems, cooling loops, hydraulic equipment failures, fire suppression system malfunctions, HVAC condensate overflow, roof leaks, and domestic plumbing failures.
Point sensors detect water at specific locations, rope sensors monitor linear areas, and flow monitoring identifies consumption anomalies indicating leaks anywhere in distribution systems. Comprehensive water leak detection coverage addresses all significant water sources within manufacturing facilities.
How does water leak detection reduce insurance costs for manufacturing facilities?
Insurance companies offer premium discounts of 5-15% for manufacturing facilities with water leak detection systems, recognizing that monitoring dramatically reduces claim frequency and severity.
Beyond premium reductions, water leak detection improves claims outcomes through documentation that supports claim validity and accelerates processing. Some insurers now require water leak detection for coverage of high-value facilities, and facilities without monitoring may face coverage limitations or higher deductibles.
Where should water leak sensors be placed in manufacturing facilities?
Strategic water leak detection sensor placement in manufacturing facilities prioritizes high-value equipment protection, critical system monitoring, and vulnerable area coverage.
Key locations include beneath CNC machines and production equipment, near hydraulic power units and process water equipment, in electrical rooms and control panel areas, at HVAC air handler condensate collection points, along fire sprinkler system risers, in loading dock areas prone to roof leaks, and beneath water heaters and domestic plumbing fixtures.
Can water leak detection prevent mold growth in manufacturing facilities?
Water leak detection directly prevents mold growth by enabling response within the critical 24-48 hour window before mold colonization begins. According to EPA guidelines, mold can begin growing on wet materials within 24-48 hours of water exposure.
Manufacturing facilities that detect and remediate leaks within this window avoid mold contamination entirely. Without leak detection, water damage often goes unnoticed for days or weeks, virtually guaranteeing mold growth that requires expensive remediation and potential facility closure.
What is the typical ROI timeline for manufacturing water leak detection systems?
Most manufacturing facilities achieve positive ROI from water leak detection within 12-24 months through combined insurance premium reductions and avoided damage costs.
Insurance savings of 5-15% on property premiums typically recover system costs within 2-3 years through premium reductions alone. When factoring in avoided damage where detected leaks average under $50,000 in losses compared to $500,000 or more for undetected incidents, payback accelerates significantly.
How do water leak detection systems integrate with manufacturing building systems?
Modern water leak detection systems integrate with building automation systems, manufacturing execution systems, and enterprise monitoring platforms through standard protocols and APIs.
Integration enables automated responses including water shutoff valve activation, equipment shutdown sequences, sump pump activation, and alarm system coordination. Alert notifications route through existing communication channels to reach appropriate personnel through text, email, phone, or facility paging systems.
What environmental conditions affect water leak sensor performance in manufacturing?
Manufacturing environments often include temperature extremes, high humidity, chemical exposure, electromagnetic interference, and physical hazards that can affect sensor performance if not addressed during system design.
Industrial-grade water leak detection sensors rated for specific environmental conditions ensure reliable performance. Site surveys during design identify challenging areas requiring specialized equipment or installation approaches, and mesh networking or wired communication options address electromagnetic interference concerns.
Protect Your Manufacturing Operations from Water Damage
Stop water damage before it stops your production. Envigilance provides 24/7 water leak detection with instant alerts, protecting your equipment, inventory, and operations from costly downtime.
Your free facility assessment includes:
- Complete water risk assessment for your manufacturing facility
- Sensor placement recommendations for maximum protection
- Integration options with your existing building systems
- ROI analysis based on your facility’s specific risk profile
- Insurance documentation support for premium reductions
Email us at detect@envigilance.com | We reply within 24 hours