Manufacturing Water Leak Detection: Stop $500K+ Damage

The maintenance director at a 400,000 square foot automotive components plant arrived Monday morning to discover extensive weekend flooding in the production area. A failed pressure relief valve on the process cooling system had released thousands of gallons of water across the manufacturing floor, damaging precision equipment, destroying inventory, and forcing a three-day production shutdown. The incident cost $380,000 in equipment repairs, lost production revenue, and emergency remediation—all preventable if automated manufacturing water leak detection had identified the failing valve before the catastrophic failure occurred. Advanced manufacturing water leak detection systems detect developing problems days or weeks before failures, enabling proactive repairs during scheduled maintenance windows.
Manufacturing facilities face unique water damage risks that differentiate industrial operations from commercial buildings. Process cooling systems, compressed air condensate lines, boiler rooms, emergency safety showers, and production equipment all create potential leak sources throughout facilities operating 24/7. According to insurance industry data, manufacturing water damage incidents cost between $25,000 and $500,000 per occurrence, with boiler room flooding alone causing $25,000-100,000 in damage when safety valves fail or pipes burst during after-hours periods when no one is present to respond. Comprehensive facility management must address water damage risks alongside energy optimization to protect operational continuity.
Manufacturing water leak detection transforms industrial facility protection through IoT-based sensor networks that monitor critical plumbing and equipment locations continuously. Modern systems detect leaks within seconds of occurrence, generate immediate alerts to maintenance teams regardless of time or day, and prevent the escalating damage that occurs when water flows undetected for hours or days. Smart water leak detection becomes essential infrastructure when a single undetected leak can cause production disruptions costing more than the entire monitoring system investment.
Manufacturing water leak detection prevents $25,000-500,000 damage incidents through 24/7 monitoring that detects leaks in seconds and enables immediate response before catastrophic failures occur.
Maximum Damage Prevented | Single Incident Protection
Leak Detection Speed | Immediate Alert Generation
Complete Deployment Timeline | No Production Downtime
Call (888) 812-1971
24/7 Monitoring | Instant Alerts | Multi-Location Support
Understanding the water damage vulnerability in manufacturing operations reveals why proactive leak detection has become essential for protecting production capacity, equipment investments, and operational continuity in industrial facilities.
Why Manufacturing Facilities Need Water Leak Detection
Manufacturing facilities operate with complex water systems that extend far beyond basic plumbing. Process cooling loops maintain precision equipment temperatures, compressed air systems generate condensate requiring drainage, boiler systems provide heating and process steam, emergency safety equipment includes overhead showers and eyewash stations, and production processes themselves often involve water in cleaning, cooling, or manufacturing operations. Each of these systems represents a potential leak source that can cause significant damage when failures occur during unattended periods. Comprehensive manufacturing water leak detection addresses all these vulnerability points through strategic sensor placement at critical monitoring locations throughout industrial facilities.
The 24/7 operating schedule common in manufacturing creates extended vulnerability windows when facilities run with minimal supervision. Weekend and overnight shifts typically operate with skeleton crews focused on production rather than facility monitoring. Small leaks that begin Friday evening can flow undetected through entire weekends, causing escalating damage with each passing hour. By Monday morning, what started as a minor drip has flooded production areas, damaged equipment, destroyed inventory, and created safety hazards requiring immediate remediation before operations can resume. Hidden building problems compound when water damage goes undetected in areas not routinely inspected during production shifts, while comprehensive facility monitoring provides the 24/7 oversight that prevents catastrophic damage incidents.
Equipment density in manufacturing environments amplifies water damage costs compared to commercial buildings. Production machinery, electronic controls, inventory, and finished goods all concentrate in relatively small areas where a single water leak can affect multiple high-value assets simultaneously. A leak above production equipment damages both the machinery and the products being manufactured. Flooding in electrical rooms affects entire facility operations beyond the immediate water damage location. According to the Insurance Information Institute, water damage represents one of the most common and costly property insurance claims across all facility types, with commercial claims often exceeding $100,000 per incident. The cascading impact of manufacturing water damage events explains why incidents regularly exceed $100,000 even when the actual leak source is relatively minor.
Production downtime represents the hidden cost of water damage that often exceeds direct repair expenses. When manufacturing facilities must shut down for water remediation, emergency repairs, and equipment replacement, the lost production revenue compounds rapidly. Automotive suppliers face penalties for missed deliveries, food processors lose entire batches of product, and electronics manufacturers cannot recover time-sensitive production schedules. The opportunity cost of downtime makes preventive leak detection far more valuable in manufacturing than in commercial buildings where business interruption costs are lower.
Insurance implications add another dimension to water leak prevention in industrial facilities. Manufacturing property insurance policies typically include substantial deductibles for water damage claims, meaning facilities absorb significant costs before insurance coverage activates. Multiple claims can trigger premium increases or policy non-renewal that affects facility viability. Environmental compliance issues emerge when water damage involves chemicals, oils, or other substances stored in manufacturing areas. Comprehensive facility monitoring that includes water leak detection demonstrates proactive risk management that insurers value and regulators expect in modern industrial operations.
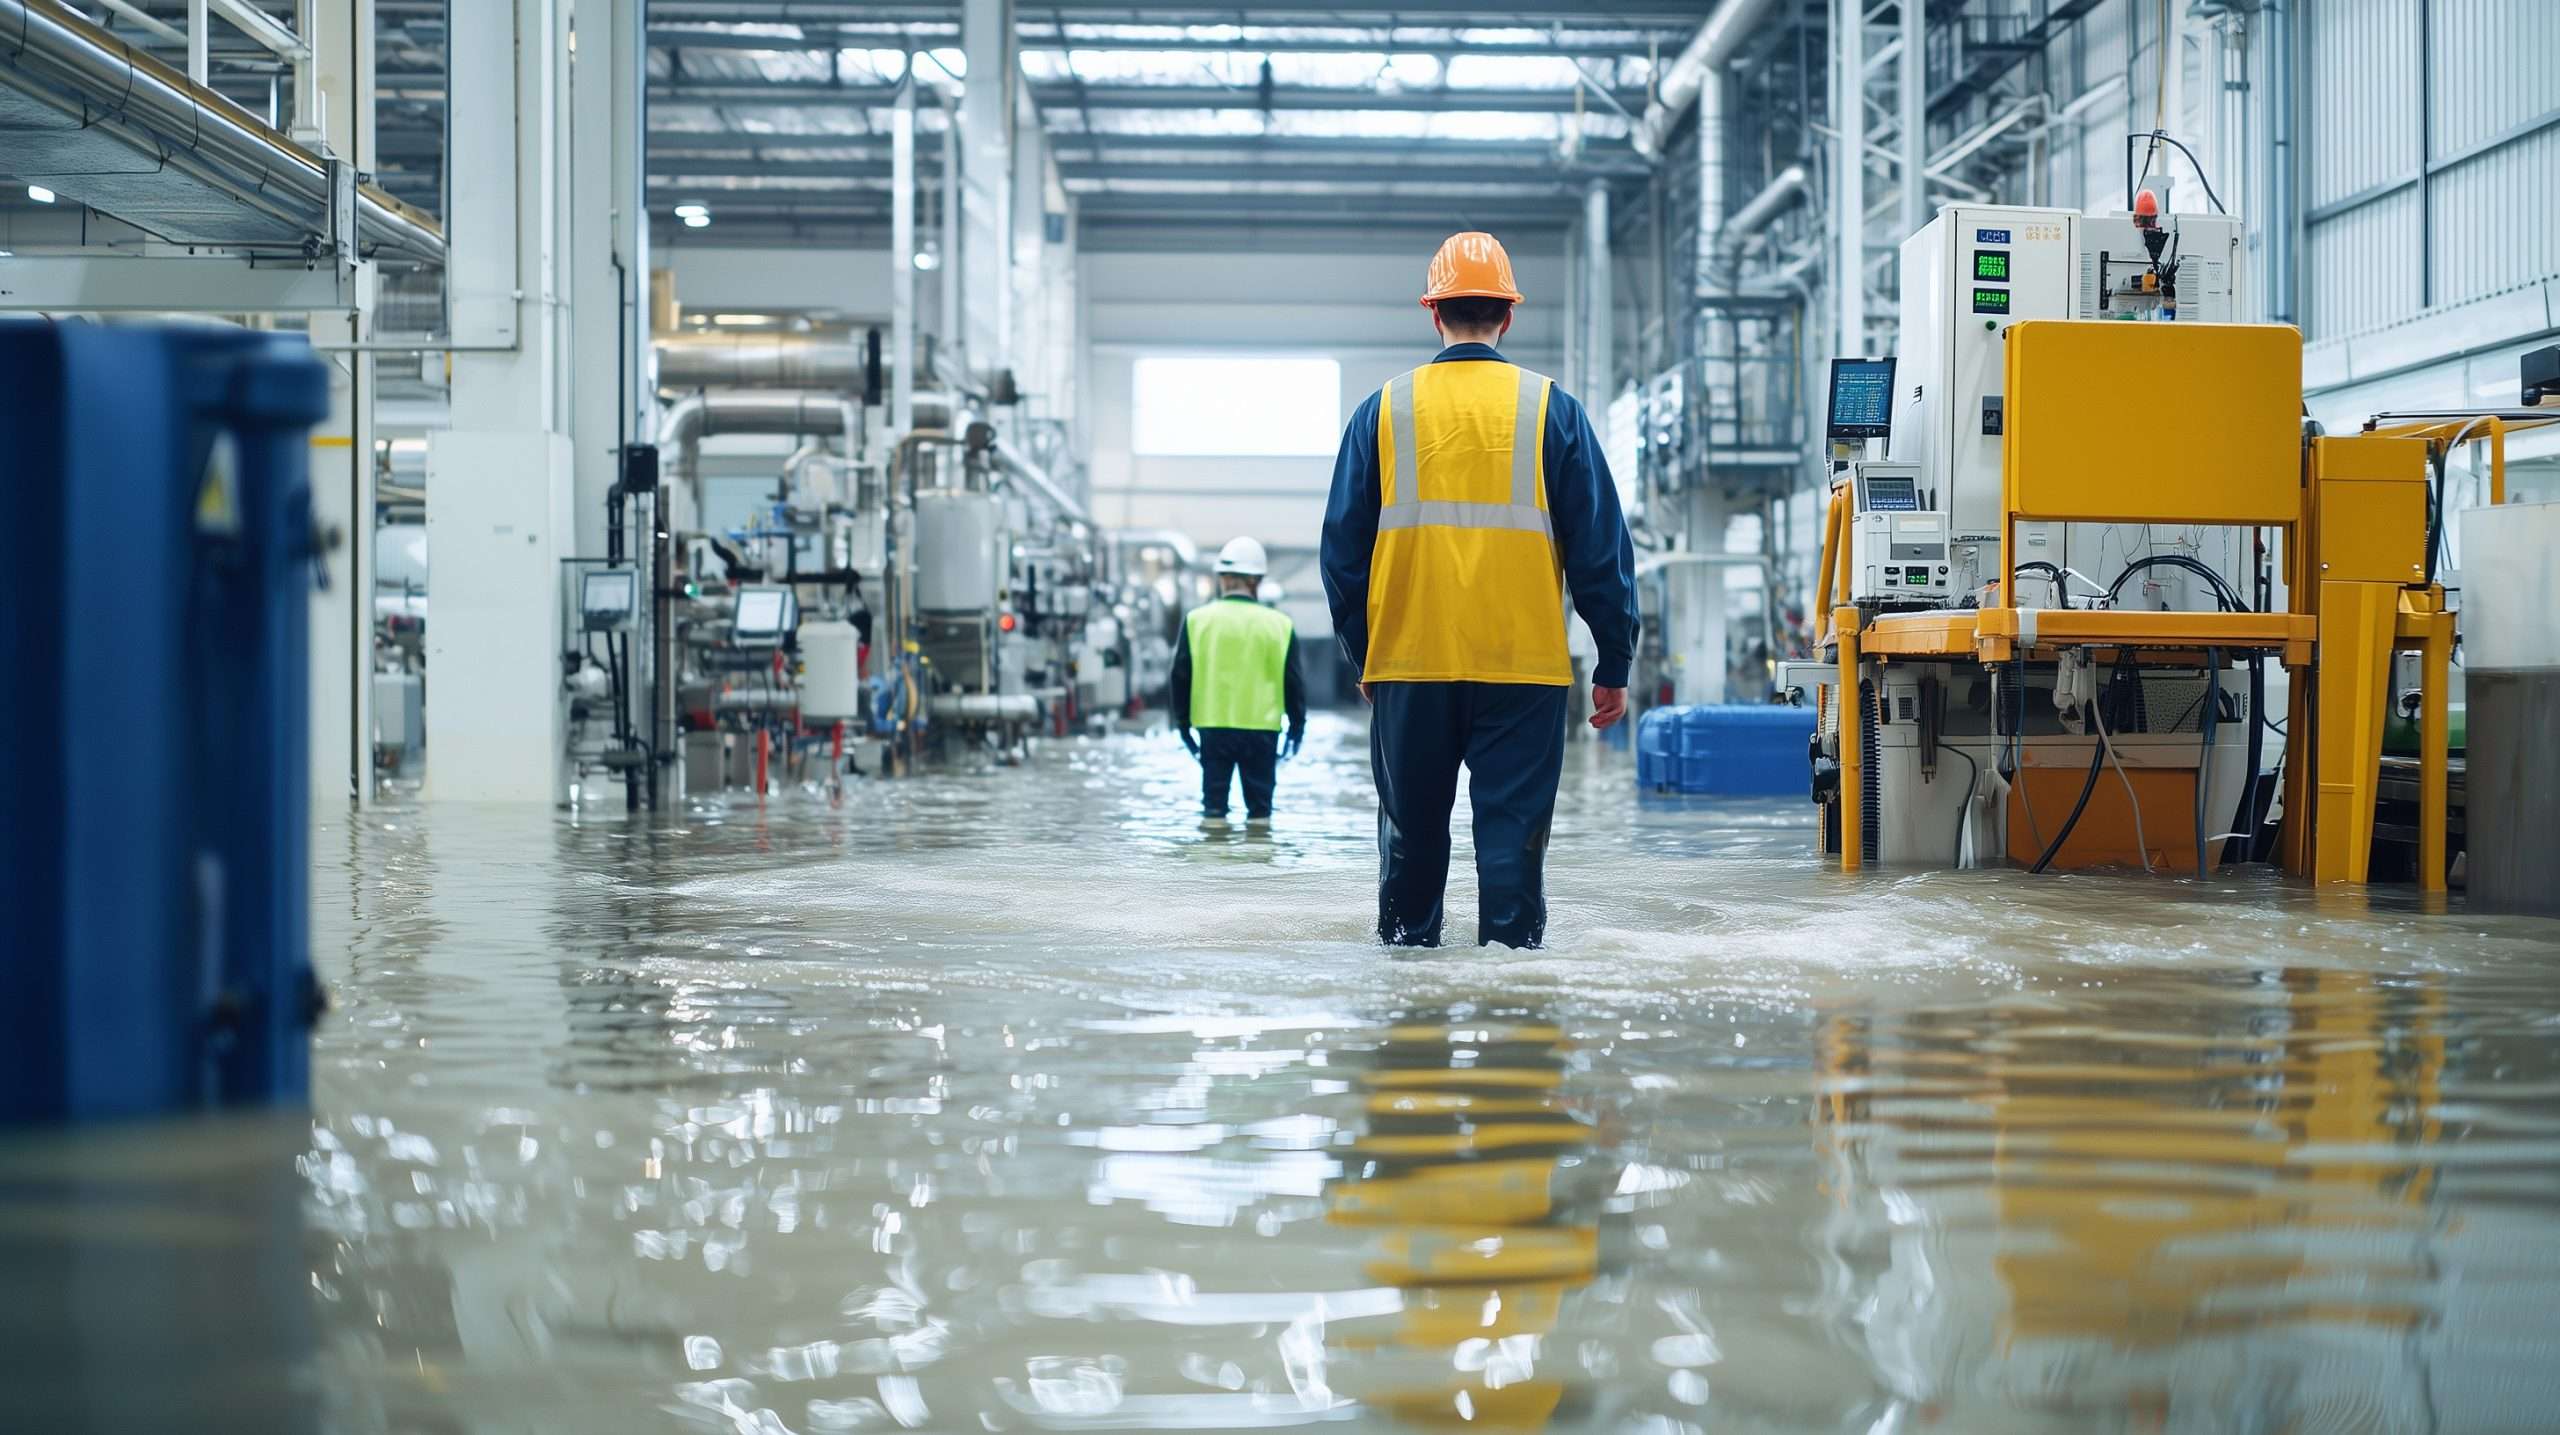
Wireless water leak detection sensors deploy at critical monitoring points throughout manufacturing facilities, detecting leaks within seconds and alerting maintenance teams immediately.
How Manufacturing Water Leak Detection Works
Manufacturing water leak detection systems deploy wireless sensors at critical monitoring points throughout industrial facilities. Sensors install near process cooling equipment, boiler rooms, compressed air system condensate drains, emergency safety shower locations, production equipment water connections, and anywhere plumbing or water-using equipment creates potential leak risk. The wireless manufacturing water leak detection sensors detect moisture through conductive sensing that triggers within seconds when water contact occurs, eliminating the hours or days of undetected flow that characterize traditional visual inspection approaches. Advanced manufacturing water leak detection technology provides continuous monitoring that never misses leaks regardless of when they occur.
Immediate alert generation represents the critical advantage of automated manufacturing water leak detection over periodic facility rounds. When sensors detect moisture, they transmit alerts via secure wireless protocols to cloud-based manufacturing water leak detection platforms that immediately notify designated personnel through text messages, phone calls, email, or mobile app notifications. Maintenance teams receive specific location information identifying exactly which sensor detected the leak, enabling rapid response without time wasted searching for leak sources. The manufacturing water leak detection notification system operates 24/7 regardless of whether facilities staff are on-site, ensuring weekend and overnight leaks receive immediate attention rather than going undetected until the next business day.
Strategic sensor placement maximizes leak detection coverage while minimizing deployment costs. Manufacturing water leak detection specialists identify high-risk locations during facility assessments—areas where leaks are most likely to occur, where damage potential is greatest, and where early detection provides maximum value. Boiler rooms receive dense sensor coverage given the high leak probability and damage potential. Critical equipment monitoring areas get priority placement to protect production machinery. Emergency response equipment locations receive sensors to ensure safety systems remain operational. Comprehensive facility management integrates water leak detection with energy monitoring and air quality systems for unified facility protection. The layered approach provides comprehensive protection without requiring sensors at every possible leak location.
Integration with facility management systems extends leak detection value beyond immediate alerts. Manufacturing water leak detection platforms connect with building automation systems, maintenance management software, and security monitoring platforms to enable coordinated responses. When major leaks occur, integrated systems can trigger automated responses including shutting off water supplies, activating sump pumps, or notifying emergency response teams. Historical leak data informs maintenance planning, identifies recurring problem areas requiring system upgrades, and documents facility conditions for insurance and compliance purposes. Equipment temperature monitoring and energy management systems integrate seamlessly with water leak detection for comprehensive facility protection.
Scalability supports phased deployment and multi-facility operations. Manufacturing organizations can begin with high-priority areas and expand coverage as budgets allow and value is demonstrated. Facilities operating multiple locations consolidate leak detection monitoring into unified dashboards providing enterprise-wide visibility. When leaks occur at any location, appropriate local teams receive immediate notification while corporate management maintains awareness of facility conditions across the entire manufacturing network through centralized reporting and alert management capabilities. Multi-facility monitoring platforms integrate water leak detection with environmental monitoring and energy management systems for comprehensive operational intelligence across entire facility networks.
6 Ways Manufacturing Water Leak Detection Protects Operations
Prevent Equipment Damage and Production Loss
Production equipment represents significant capital investment vulnerable to water damage from overhead leaks, flooding, or moisture infiltration. Manufacturing water leak detection enables rapid response before water reaches critical equipment or production areas. Early intervention through manufacturing water leak detection prevents equipment damage, protects inventory and finished goods, and avoids the production downtime required for water remediation and equipment replacement. Facilities report that single prevented incidents often justify years of manufacturing water leak detection system costs through avoided equipment damage and production loss.
Protect Boiler Rooms and Mechanical Spaces
Boiler rooms concentrate multiple water damage risks including pressure relief valve failures, pipe corrosion, condensate drain overflow, and system pressure fluctuations that cause leaks. These areas typically operate unattended with minimal supervision, allowing leaks to flow for extended periods before detection. Manufacturing water leak detection provides continuous boiler room monitoring with immediate alerts when moisture appears, preventing the $25,000-100,000 damage incidents that characterize boiler room flooding events. Protected facilities maintain operational continuity rather than facing emergency shutdowns when critical heating or process steam systems fail due to water damage. Comprehensive manufacturing water leak detection coverage in mechanical spaces represents essential infrastructure protection for continuous manufacturing operations.
Monitor Process Cooling System Integrity
Process cooling systems maintain temperature-sensitive manufacturing equipment but create leak vulnerability through extensive piping networks, connections, and pressure variations. Cooling system failures can damage both the plumbing infrastructure and the production equipment depending on cooling. Temperature monitoring combined with water leak detection provides comprehensive protection for process cooling operations. Early leak detection enables repair scheduling during planned maintenance rather than emergency response during production runs, while preventing the equipment overheating that occurs when cooling system failures go undetected.
Enable After-Hours Protection
Weekend and overnight periods represent maximum water damage vulnerability when facilities operate with minimal supervision focused on production rather than building monitoring. Manufacturing water leak detection eliminates reliance on visual inspection during unattended periods by providing continuous automated monitoring that never requires human presence. Maintenance teams receive immediate manufacturing water leak detection alerts regardless of time or day, enabling rapid response to weekend leaks before Monday morning arrives with catastrophic damage requiring emergency remediation and production shutdowns. The 24/7 manufacturing water leak detection protection addresses the reality that water damage events do not occur conveniently during staffed business hours.
Support Insurance and Compliance Requirements
Manufacturing property insurance increasingly expects proactive risk management including water damage prevention systems. Leak detection demonstrates due diligence that can influence premium rates, deductibles, and policy terms. When claims do occur, documented monitoring systems and rapid response timelines support favorable claim outcomes by showing appropriate preventive measures and damage mitigation efforts. Comprehensive facility monitoring including water leak detection creates documentation supporting regulatory compliance, insurance requirements, and corporate risk management programs.
Protect Multi-Location Manufacturing Networks
Manufacturing organizations operating multiple facilities gain enterprise-wide water damage protection through centralized leak detection platforms. When leaks occur at any location, local maintenance teams receive immediate alerts while corporate management maintains visibility across the entire facility network. Consolidated reporting identifies facilities requiring plumbing infrastructure upgrades, tracks water damage prevention performance across locations, and supports capital planning for proactive system replacements. The unified approach provides consistent protection standards regardless of individual facility staffing or local management attention to building maintenance.
Real Results from Manufacturing Facilities
Manufacturing facilities implementing manufacturing water leak detection consistently report prevented damage incidents that justify system investments many times over. A 500,000 square foot food processing facility prevented $280,000 in damage when manufacturing water leak detection sensors identified a failing cooling system valve at 2:00 AM on Saturday morning. The maintenance team responded within 30 minutes, shutting off water supply and initiating repairs that completed during the planned weekend maintenance window. Without manufacturing water leak detection, the valve would have failed completely over the weekend, flooding production areas and requiring week-long shutdown for emergency remediation and equipment replacement.
Insurance benefits extend beyond prevented claims to include premium reductions and improved policy terms. Carriers recognize proactive water damage prevention as effective risk mitigation that reduces their exposure to large loss events. Manufacturing facilities with documented leak detection systems report 10-20% premium reductions on property insurance, with payback periods of 2-4 years even without accounting for prevented damage incidents. The combination of avoided claims and reduced premiums creates compelling financial justification independent of operational continuity benefits. The EPA WaterSense program encourages commercial facilities to implement water management best practices including leak detection as part of comprehensive resource efficiency initiatives.
Maintenance efficiency improves when leak detection provides early warning of developing plumbing problems. Small leaks detected before catastrophic failures enable scheduled repairs during planned maintenance windows rather than expensive emergency service calls. Maintenance teams can order parts in advance, schedule work during production downtime, and coordinate repairs with other planned work. The transition from reactive crisis management to proactive maintenance scheduling reduces costs while improving facility reliability and equipment longevity through proper care rather than emergency patches.
Environmental compliance benefits emerge when water leak detection prevents incidents involving chemicals or regulated substances. Manufacturing facilities storing chemicals near water systems face potential environmental violations if flooding causes releases. Leak detection that prevents facility flooding eliminates the environmental compliance risks, regulatory reporting requirements, and potential fines that characterize chemical release events. The National Fire Protection Association emphasizes proactive facility protection measures including leak detection as essential components of comprehensive building safety and risk management programs. The regulatory protection adds another dimension of value beyond direct damage prevention.
Peace of mind represents the intangible benefit that manufacturing leadership values highly. Knowing that water leaks will trigger immediate alerts regardless of when they occur eliminates the anxiety about weekend discoveries of catastrophic damage. Facilities managers sleep better knowing that automated systems provide protection during unattended periods. Corporate management gains confidence that facility risk management addresses one of the most common and costly building failures affecting manufacturing operations.

Intuitive water leak detection dashboards provide instant visibility into sensor status across entire manufacturing facilities, enabling rapid response and comprehensive documentation.
Manufacturing Water Leak Detection vs. Visual Inspection
Traditional water leak detection in manufacturing relies on visual inspection during facility rounds, periodic equipment checks, and reactive response to visible water damage or equipment failures. This approach fails to protect against the weekend and overnight leaks that cause the most expensive damage incidents. Maintenance teams conducting facility rounds during business hours miss leaks that begin Friday evening and flow for 60+ hours before Monday morning discovery. The delayed detection allows minor leaks to escalate into major damage events requiring emergency remediation and production shutdowns. Manufacturing water leak detection eliminates these vulnerabilities through continuous 24/7 automated monitoring that detects problems immediately regardless of staffing levels or inspection schedules.
Detection speed differences between visual inspection and automated monitoring fundamentally change damage outcomes. Human inspection operates on daily or weekly schedules at best, with many areas receiving only monthly checks. Manufacturing water leak detection systems identify leaks within 30 seconds of occurrence, generating immediate alerts that enable response measured in minutes rather than days. The speed advantage prevents escalation from minor leaks into facility flooding, reducing damage costs by 80-95% compared to delayed detection scenarios.
Coverage consistency separates automated detection from human inspection approaches. Visual rounds depend on individual technician diligence, facility access during inspections, and visible evidence of water presence. Hidden leaks behind equipment, under floors, or in ceiling spaces go undetected until damage becomes obvious. Smart water detection systems monitor continuously regardless of accessibility, visibility, or staff attention, providing protection that human inspection cannot match regardless of inspection frequency or technician skill.
Cost effectiveness analysis reveals automated detection delivers superior protection at lower total cost than intensive visual inspection programs. Implementing comprehensive hourly inspection coverage throughout facilities would require multiple dedicated staff members working 24/7—an approach costing hundreds of thousands annually while still failing to match the immediate detection capabilities of automated systems. Manufacturing water leak detection typically costs $5,000-15,000 annually for comprehensive facility coverage, providing superior protection at a fraction of the cost that equivalent human monitoring would require.
Documentation and accountability improve with automated monitoring compared to inspection-based approaches. Leak detection systems create permanent records of when leaks occurred, how quickly teams responded, and what actions were taken. This documentation supports insurance claims, demonstrates compliance with risk management protocols, and provides objective evidence for investigating recurring problems. Visual inspection creates minimal documentation beyond inspection checklists that provide little value for incident analysis or process improvement initiatives.
Implementation Process for Manufacturing Water Leak Detection
Manufacturing water leak detection implementation begins with facility assessment identifying critical monitoring locations based on leak probability, damage potential, and operational priorities. Technical specialists evaluate plumbing infrastructure, equipment water connections, mechanical spaces, production areas, and historical leak locations to create customized manufacturing water leak detection sensor placement plans. Unlike traditional plumbing upgrades requiring extensive construction, manufacturing water leak detection assessment typically completes within hours and leads directly to rapid wireless sensor deployment without facility modifications or production interruption.
Sensor installation proceeds quickly because wireless devices require no wiring or plumbing modifications. Water detection sensors mount near floor level in areas where water would accumulate during leaks—under equipment, near drain locations, in mechanical rooms, and anywhere water systems create risk. Most manufacturing facilities complete initial deployment of 20-50 sensors within a single day, with sensors immediately beginning continuous monitoring upon activation. The non-invasive installation enables comprehensive protection without the construction work that would be required for wired detection systems.
Alert configuration tailors notification protocols to facility-specific requirements and staffing patterns. Manufacturing water leak detection platforms support multiple notification methods including text messages, phone calls, emails, and mobile app alerts. Facilities configure primary and secondary contact sequences ensuring alerts reach appropriate personnel regardless of time or day. Escalation protocols automatically notify additional team members if initial alerts go unacknowledged, preventing situations where weekend leaks continue because the first-call person is unavailable. Comprehensive monitoring systems integrate water leak detection with equipment monitoring for unified alert management across all facility systems.
Testing and training ensure system effectiveness before relying on automated detection. Installation teams verify each sensor by triggering test alerts, confirming notification delivery, and documenting sensor locations for maintenance reference. Staff training covers alert interpretation, sensor identification, and recommended response protocols. Most manufacturing facilities achieve operational readiness within hours of installation completion, with teams prepared to respond effectively when real leak alerts occur.
Expansion follows naturally as facilities recognize protection value and identify additional coverage opportunities. Areas not included in initial deployment become priorities as teams gain confidence in system effectiveness. The scalable architecture supports unlimited sensor additions without platform limitations. Many manufacturing organizations begin with highest-risk areas including boiler rooms and critical equipment, progressively expanding to comprehensive facility coverage as budgets allow and demonstrated value justifies continued investment in proactive water damage prevention.
Choosing the Right Manufacturing Water Leak Detection Provider
Manufacturing facility managers evaluating manufacturing water leak detection providers should prioritize several key factors distinguishing effective solutions from inadequate alternatives. Industrial experience matters because manufacturing environments involve equipment types, operational patterns, and facility challenges that generic building leak detection cannot address effectively. Providers with demonstrated success in manufacturing water leak detection understand process cooling systems, boiler operations, compressed air condensate management, and the 24/7 operational requirements that differentiate industrial facilities from commercial buildings.
Sensor durability and industrial-grade construction are essential for manufacturing environments involving dust, chemicals, temperature extremes, and physical impacts that would damage consumer-grade sensors. Manufacturing water leak detection sensors should feature waterproof enclosures, chemical-resistant materials, and rugged construction suitable for industrial conditions. The sensors must function reliably in harsh environments over multi-year service lives without requiring frequent replacement or generating false alerts from environmental conditions unrelated to actual leaks.
Alert reliability represents the most critical system characteristic because missed alerts eliminate protection value entirely. Monitoring platforms should provide redundant notification methods, cellular backup connectivity ensuring alerts transmit during network outages, and confirmation systems verifying alert delivery to intended recipients. Providers offering 24/7 technical support enable rapid troubleshooting when alert system questions arise, ensuring facilities maintain continuous protection rather than discovering communication failures when actual leaks occur.
Multi-facility support capabilities matter for manufacturing organizations operating multiple locations. Water leak detection platforms should provide centralized monitoring dashboards, consolidated reporting across facility networks, and standardized sensor management regardless of location. Corporate management gains visibility into water damage protection across the entire organization while local maintenance teams retain direct access to facility-specific sensors and alert configurations. The unified approach enables consistent protection standards across facilities with varying local management capabilities.
Total cost of ownership should include not just initial sensor costs but ongoing subscription fees, sensor replacement expectations, technical support availability, and platform upgrade paths. Subscription-based models with predictable monthly costs provide better budget management than systems requiring large upfront investments plus unpredictable maintenance expenses. Manufacturing organizations should evaluate complete financial pictures including installation, monitoring fees, sensor longevity, and expansion costs as facility needs evolve. Hidden costs emerging after deployment undermine project economics and prevent organizations from achieving comprehensive protection across all critical areas. Comprehensive facility protection requires transparent pricing and realistic long-term cost projections.
Frequently Asked Questions About Manufacturing Water Leak Detection
How many sensors does a typical manufacturing facility require?
Sensor requirements vary based on facility size, plumbing complexity, and risk concentration, but typical 200,000-400,000 square foot manufacturing facilities deploy 30-60 sensors for comprehensive manufacturing water leak detection coverage. High-risk areas including boiler rooms, mechanical spaces, and critical equipment locations receive multiple sensors for redundant manufacturing water leak detection protection, while lower-risk areas may require only strategic placement at key monitoring points. Facility assessments identify optimal sensor quantities balancing comprehensive manufacturing water leak detection protection with reasonable deployment costs. Phased installation enables facilities to begin with highest-priority areas and expand coverage as budgets allow.
Can sensors detect slow leaks before significant damage occurs?
Water leak detection sensors trigger when moisture contacts sensing elements, detecting even small leaks that produce minimal water flow. Slow drips accumulate over time creating puddles or moisture that activates nearby sensors long before damage becomes extensive. Strategic sensor placement in areas where water naturally flows or accumulates ensures even minor leaks generate alerts before escalating into major problems. The early detection capability provides time for planned repairs rather than emergency response, preventing the damage progression that occurs when slow leaks continue undetected for weeks or months.
What happens if sensors generate false alerts?
Industrial-grade leak detection sensors are specifically designed to minimize false alerts through moisture-specific sensing technology that distinguishes between water leaks and environmental humidity. Proper sensor placement away from cleaning operations, condensation sources, and high-traffic areas further reduces false alert probability. When alerts occur, facilities investigate to verify actual leaks versus environmental factors. Occasional false alerts represent minimal burden compared to the catastrophic damage prevented by real leak detection, though quality systems typically maintain false alert rates below 5% of total notifications.
Does installation require production downtime?
Wireless water leak detection deploys with zero production interruption through battery-powered sensors that mount without electrical work, plumbing modifications, or facility alterations. Installation teams place sensors during normal operations in minutes per location without affecting production equipment or manufacturing processes. Most facilities complete comprehensive sensor deployment within a single day while maintaining full production schedules. The non-invasive installation represents a fundamental advantage over traditional building monitoring systems requiring construction work and equipment downtime.
How does monitoring work during network or power outages?
Quality water leak detection systems include cellular backup connectivity ensuring alert transmission continues during local network outages. Battery-powered sensors operate independently of facility electrical systems, maintaining detection capability during power failures. When connectivity restores, systems transmit any missed events and confirm operational status. The redundant architecture ensures continuous protection regardless of facility infrastructure conditions, addressing the reality that water leaks often occur during the same weather events or utility disruptions that affect electrical and network services.
Can systems integrate with existing facility management platforms?
Modern leak detection platforms integrate with building automation systems, computerized maintenance management software, and facility monitoring platforms through standard APIs. Integration enables automated responses when leaks occur including shutting off water supplies, activating pumps, or triggering security protocols. Leak event data flows into maintenance management systems for work order generation and historical tracking. The connected approach maximizes response effectiveness while maintaining comprehensive documentation for insurance, compliance, and continuous improvement purposes.
What maintenance do sensors require?
Water leak detection sensors are designed for multi-year operation with minimal maintenance requirements. Battery-powered sensors typically operate 3-5 years before battery replacement, with platforms providing advance warning when battery levels decline. Periodic sensor testing using water contact verification ensures operational readiness. Physical cleaning may be required if sensors accumulate dust or debris in industrial environments. The low-maintenance design enables facilities to maintain comprehensive protection without significant ongoing effort or recurring maintenance costs beyond occasional battery replacements included in subscription pricing.
What is the typical ROI timeline?
Most manufacturing facilities achieve positive ROI within the first prevented damage incident, which typically occurs within 12-24 months of deployment. The $25,000-500,000 costs of manufacturing water damage incidents exceed comprehensive leak detection system investments by factors of 5-50 times. Even without considering prevented incidents, insurance premium reductions of 10-20% often deliver payback within 2-4 years. The combination of damage prevention, insurance benefits, and maintenance efficiency improvements creates compelling financial justification with rapid payback and substantial ongoing value.
Protect Your Manufacturing Facility from Water Damage
Manufacturing water leak detection provides the 24/7 protection your facility needs to prevent catastrophic damage, avoid production disruptions, and maintain operational continuity. Every day without automated leak detection represents vulnerability to weekend flooding that could cost hundreds of thousands in emergency repairs and lost production revenue.
Your free facility assessment includes:
✓ Comprehensive risk assessment identifying critical monitoring locations
✓ Sensor placement recommendations based on leak probability and damage potential
✓ Implementation timeline with zero production downtime
✓ Alert configuration for 24/7 maintenance team notification
✓ ROI analysis including insurance benefits and prevented damage costs
Email us at detect@envigilance.com | We reply within 24 hours
Related Industries
Water damage threatens all types of facilities. Discover how other industries protect operations through comprehensive water leak detection: